

Threaded titanium components offer unmatched strength-to-weight performance, yet the material properties that make titanium so valuable in demanding applications also make its threads exceptionally unforgiving. In standard aerospace alloys like Ti-6Al-4V, poor thermal dissipation, elastic springback during machining, and a strong tendency toward adhesive wear routinely turn standard assembly into seized hardware, damaged thread flanks, or scrapped precision parts. Because titanium shear strength runs roughly 60% of its ultimate tensile strength, standard fastener formulas built for steel often lead to joint failure. This guide breaks down the physical mechanisms behind galling and thread stripping, details how engagement length and tolerances dictate joint integrity, and outlines practical design controls to protect your assemblies.
Why Titanium Threaded Features Fail
Titanium alloys see widespread use in aerospace structures, medical implants, and high-performance automotive systems where mass reduction and corrosion resistance are non-negotiable. However, cutting or forming internal and external threads in titanium introduces steep manufacturing and field performance risks. Scrapping an intricate aerospace housing late in production due to a galled tapped hole is a costly error. Without strict design tolerances and proper surface preparation, titanium threads frequently suffer catastrophic failure during torque-down or service maintenance.
How Titanium Properties Affect Threads
The physical behavior of titanium works directly against smooth thread engagement. Under high contact pressure, titanium tends to adhere to mating metals due to its chemical reactivity. During fastener installation, sliding friction easily ruptures titanium’s microscopic, passive oxide layer ($TiO_2$). Once exposed, the highly reactive bare metal cold-welds to the mating thread flank on contact.
Thermal behavior compounds this issue. Industry-standard Ti-6Al-4V exhibits a thermal conductivity of roughly 6.7 W/m·K, a fraction of carbon steel’s 45 W/m·K. Because heat cannot escape through the component body during rapid fastener installation, localized temperatures spike rapidly at the thread interface. This sudden thermal expansion increases contact pressure, breaking down temporary lubricants and locking the threads solid. Furthermore, titanium’s lower elastic modulus (~114 GPa versus ~200 GPa for steel) leads to elastic deformation under load, causing the thread material to spring back and binding against mating hardware.
Key Failure Modes: Galling vs. Stripping
Galling and thread stripping represent two distinct structural failure mechanisms in titanium fastening systems:
- Galling (Adhesive Wear): Frictional heating and surface pressure cause asperities on opposing thread flanks to micro-weld. As rotation continues, these welds tear away chunks of raw metal, creating heavy scoring. The fastener seizes fast—often long before reaching the required torque preload. Once locked, removing the bolt typically shears the shank or shreds the internal hole entirely.
- Thread Stripping (Shear Failure): Stripping occurs when applied tensile or torque loads exceed the shear capacity of the thread form. Although Ti-6Al-4V boasts high tensile strength (~950–1000 MPa), its shear strength is significantly lower—typically capped at 60% of tensile capability. If internal thread engagement depth is shallow or root clearances are oversized, the bolt strips the internal titanium material clean out of the wall.
How to Prevent Galling and Thread Stripping
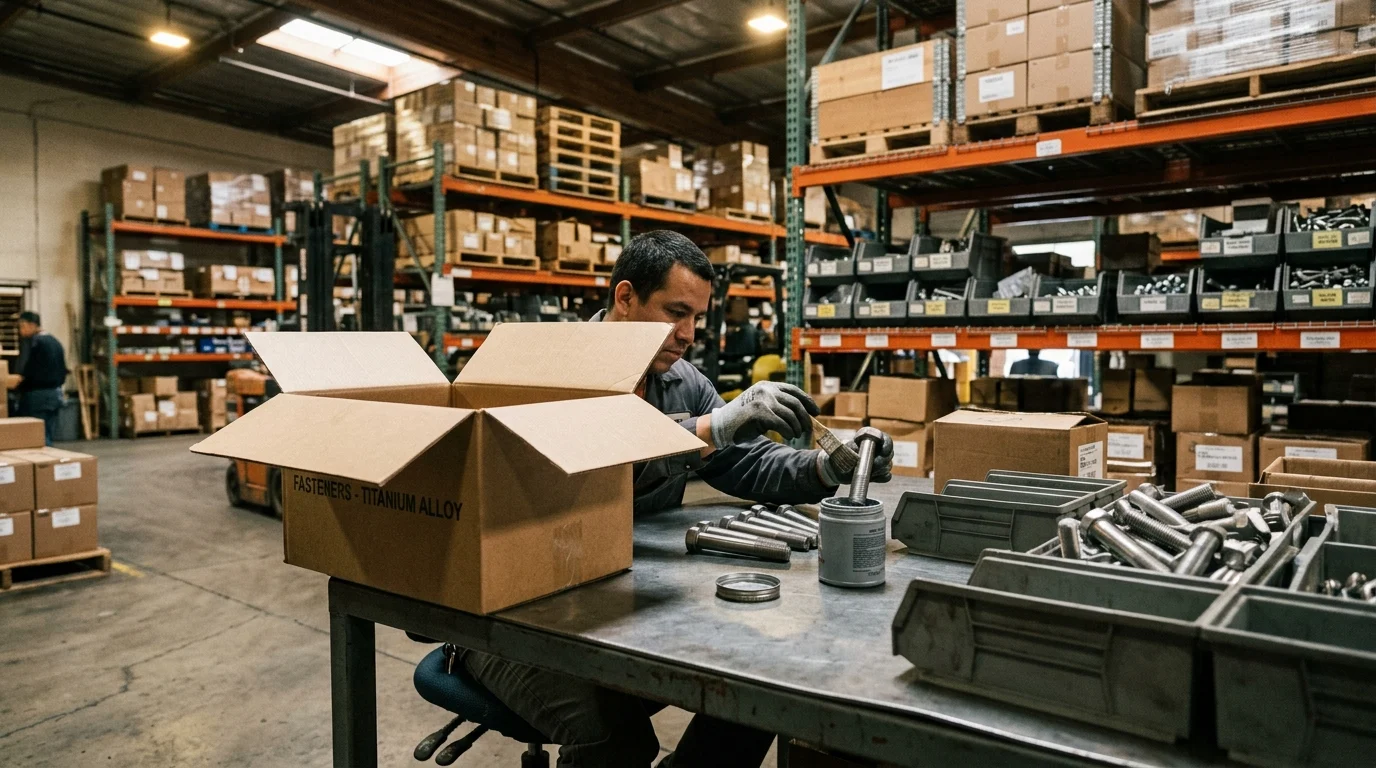
Preventing thread seizure and shear failure requires balancing thread geometry, mechanical engagement depths, and barrier coatings rather than relying on standard hardware catalog defaults.
Thread Form, Engagement Length, and Tolerances
Steel thread rules do not translate directly to titanium. To account for lower shear strength, engineers should increase thread engagement depth. Where a 1.0D to 1.5D depth (D = nominal fastener diameter) works in steel or iron, titanium internal threads generally require 1.5D to 2.0D engagement. This extra depth spreads shear stress over more thread crests, preventing load concentration on the first two engaged threads.
Tolerance class selection directly influences galling risks. Specifying tight Class 3B (internal) or Class 3A (external) threads leaves almost zero radial clearance for thermal expansion or liquid/dry-film lubricants. Switching to Class 2B/2A tolerances provides needed relief, allowing solid film coatings or anti-seize pastes to sit on the thread flank without binding. For dynamic or high-fatigue joints, specifying UNJ/UNJR thread profiles with enlarged, controlled root radii mitigates sharp stress risers that trigger fatigue cracking.
Inserts, Surface Treatments, and Lubrication
Bare titanium-on-titanium contact should be avoided whenever possible in reusable or dynamic joints. Utilizing stainless steel thread inserts (such as Nitronic 60 helical coils or A286 solid key-locking inserts) creates a hard, gall-resistant interface while reinforcing the softer host metal.
Where physical inserts are impractical due to space or weight limits, specialized surface treatments and coatings are required to prevent metal-to-metal contact:
| Treatment / Coating | Typical Friction Coeff. (µ) | Primary Advantage | Best Applied To |
|---|---|---|---|
| Bare Ti-6Al-4V | 0.35 – 0.45 | Uncoated baseline | Static, single-use joints only |
| AMS 2488 Type II Anodizing | 0.20 – 0.25 | Converts oxide surface; prevents bare metal contact | Moderate load aerospace threads |
| PVD Titanium Nitride (TiN) | 0.40 – 0.50 | Hard surface layer; prevents galling against steel | Requires secondary paste/dry film |
| Diamond-Like Carbon (DLC) | 0.05 – 0.15 | Extreme lubricity; dry-running wear protection | High-cycle or vacuum-environment threads |
Regardless of coating choice, wet assembly protocols should specify molybdenum disulfide ($MoS_2$) dry-film lubes or silver-based anti-seize pastes to stabilize torque-tension relationships. During assembly shop floor execution, operators should run down titanium hardware at low speeds, avoiding high-RPM impact drivers that generate instant frictional heat spikes.
How to Validate and Source Titanium Threads
Preventing field failures requires verifying thread quality long before hardware reaches the assembly bench. Thread manufacturing in titanium demands high-pressure coolant (HPC) during tapping or thread milling to clear stringy chips and maintain smooth surface finishes on thread flanks. Rough flank surface finishes trigger immediate galling during torque-down.
Validation protocols should include 100% thread gaging using calibrated Go/No-Go plug gages prior to applying anodizing or physical vapor deposition. For flight-critical hardware, optical comparators or pitch micrometer inspections are recommended to confirm UNJ root radii and pitch diameter tolerances. Sourcing titanium threaded components from suppliers experienced in titanium DFM ensures proper tooling geometry, low surface roughness ($Ra < 0.8 \mu m$), and controlled coating thicknesses on all threaded features.
💡 Designing Threaded Titanium Parts or Resolving Fastener Galling?
We manufacture custom titanium CNC machined and 3D printed components equipped with precision-milled UNJ threads, Nitronic inserts, and AMS 2488 Type II anti-galling surface finishes.Upload CAD Models for Free DFM & Engineering Review
Key Takeaways
- Extend engagement length to 1.5D–2.0D in titanium holes to distribute shear loads and protect against thread stripping.
- Account for Ti-6Al-4V’s low thermal conductivity (~6.7 W/m·K); fast installation generates local heat that causes hardware to seize.
- Select Class 2B/2A tolerances to allow room for anti-galling coatings and thermal expansion without thread binding.
- Isolate titanium surfaces using stainless steel inserts (Nitronic 60/A286), Type II anodizing, or dry-film lubricants.
- Distinguish between galling (adhesive cold-welding) and stripping (shear overstress) during root-cause failure analysis.
Frequently Asked Questions
Why do titanium threads gall so easily?
Titanium readily adheres to mating surfaces under friction. When assembly pressure breaks the thin oxide layer, raw titanium cold-welds to opposing threads, creating heavy micro-tearing and immediate seizure.
How does titanium’s low thermal conductivity affect threaded joints?
Ti-6Al-4V conducts heat at roughly 6.7 W/m·K (versus ~45 W/m·K for carbon steel). Frictional heat generated during fastener run-down stays trapped at the thread interface, causing thermal expansion and galling.
What engagement length is best for titanium internal threads?
Internal threads in titanium should target 1.5D to 2.0D engagement depth. This longer depth offsets titanium’s lower shear strength (~60% of tensile strength) by spreading force across more thread flanks.
What is the difference between galling and thread stripping?
Galling is adhesive wear and cold-welding caused by surface friction. Thread stripping is a structural shear failure where applied force shears the thread teeth off the internal hole wall.
Why do titanium threads strip even though the material is strong?
While titanium has high tensile strength, its shear strength is only about 60% of tensile capability. Threads fail primarily under shear stress, requiring deeper engagement and wider clearances.